
- Site Navigation -
— PRODUCTS —
PRODUCT CENTER
Hot Stamping Dies for Body Structural Parts
+86 18932785670
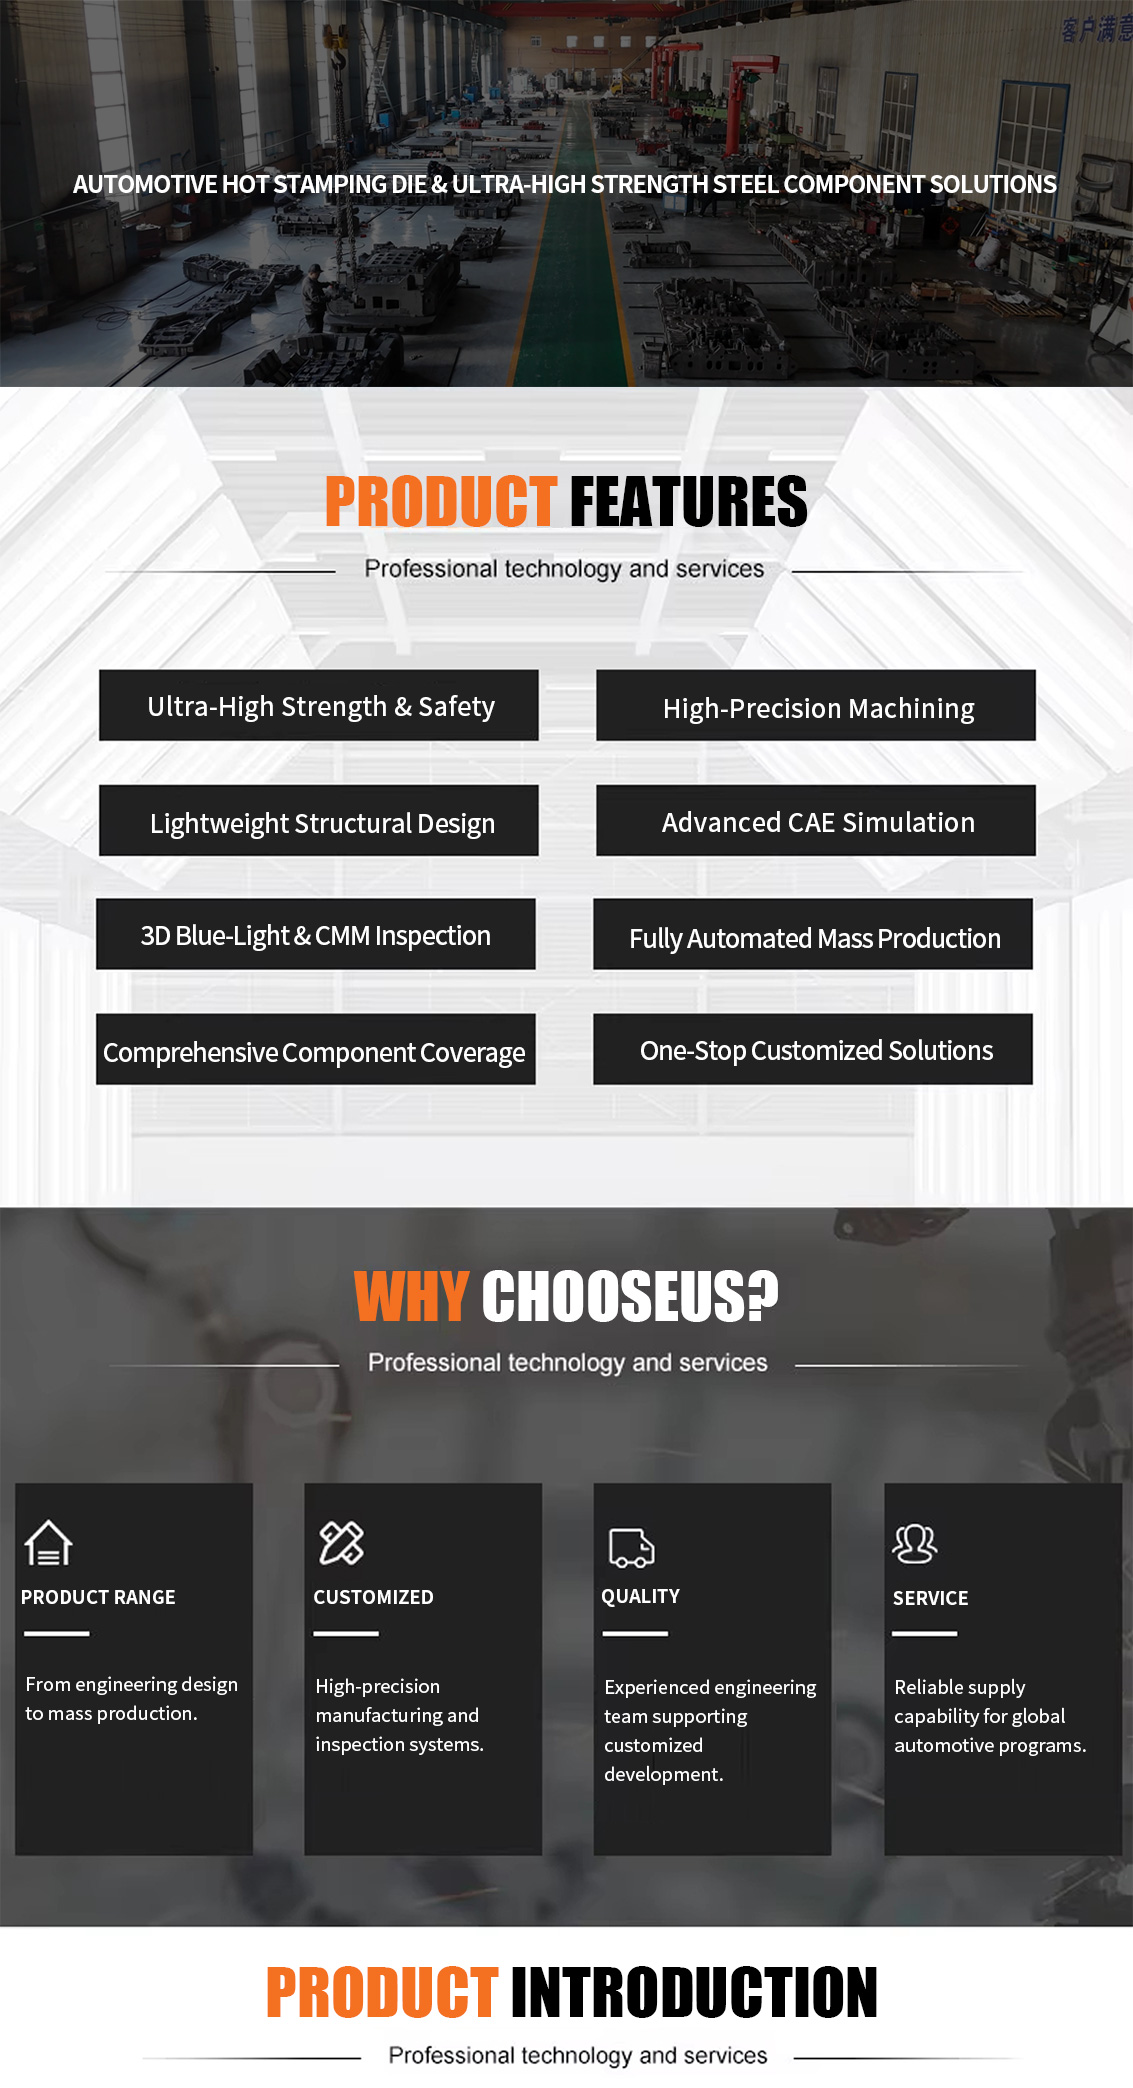
Hot Stamping Die Cooling System Design
Hebei Haoxinran Machinery specializes in the design and manufacturing of hot stamping dies with advanced cooling systems that ensure optimal quenching performance. The cooling system is the heart of any hot stamping die, directly determining the material properties, dimensional accuracy, and production efficiency of the final component. Our engineering team has developed proprietary cooling channel design methodologies that balance uniform quenching, cycle time optimization, and die durability.
Cooling Channel Engineering
The cooling channels in a hot stamping die must be precisely positioned to achieve the required quenching rate (typically above 30°C per second for boron steel martensitic transformation). Our design process begins with thermal simulation that maps heat flux distribution across the die surface. Channels are then placed strategically to match heat intensity—closer to the surface in high-heat zones and further away in areas requiring slower cooling.
Conformal Cooling Design: Cooling channels follow the die surface contour, providing uniform cooling across complex part geometries including ribs, flanges, and deep draw areas. This is critical for preventing uneven martensitic transformation that leads to part distortion and inconsistent mechanical properties.
Flow Optimization: Computational fluid dynamics (CFD) analysis ensures consistent coolant flow velocity through all channels, eliminating dead spots and hot spots. Proper flow rate prevents boiling within channels and maintains reliable heat transfer.
Channel Size and Spacing: We optimize channel diameter (typically 8-14mm) and center-to-center spacing based on die material, part geometry, and required quench rate. Too close and the die surface temperature drops too rapidly, too far and cooling becomes insufficient.
Manifold Design: Inlet and outlet manifolds are designed for balanced flow distribution across multiple cooling circuits, ensuring that all regions of the die receive appropriate coolant flow regardless of their position in the circuit.
Coolant System Specifications
Our hot stamping dies use water-based coolant systems typically operating at 20-40°C inlet temperature with flow rates calculated to achieve the required quench rate. The system includes:
High-flow circulation pump with variable speed control
Plate heat exchanger connected to plant cooling water or chiller
Temperature sensors at each inlet and outlet circuit
Pressure monitoring and flow control valves
Filtering system to prevent channel blockage
Die Material Selection for Hot Stamping
Hot stamping dies operate at elevated temperatures and undergo repeated thermal cycling. We select die materials based on the specific production volume and part requirements:
1.2343 (H11) / 1.2344 (H13): Standard hot work tool steel for moderate production volumes, good thermal conductivity and toughness.
1.2367: Higher performance hot work steel with improved thermal fatigue resistance for extended production runs.
P/M Tool Steels: Powder metallurgy steels such as Vanadis or Dura for extreme wear resistance in high-volume programs.
Die inserts are heat treated to 46-50 HRC and undergo surface treatments such as nitriding or PVD coating to reduce soldering and improve die life.
Process Validation and Tryout
Before delivery, each hot stamping die undergoes comprehensive tryout on production or tryout presses. We verify:
Part geometry and dimensional accuracy with CMM measurement
Material hardness and microstructure (hardness testing, metallography)
Cooling performance and temperature distribution
Cycle time optimization for target production rate
Surface quality and dimensional consistency over multiple cycles
Contact Hebei Haoxinran Machinery to discuss your hot stamping die cooling system requirements. We provide complete die design, manufacturing, and tryout support for automotive structural component programs.
Contact Us
- Company Name: Hebei Haoxinran Machinery Manufacturing Co.,Ltd.
- Hotline: +86 18932785670
- Email: project@haoranmj.com
- Website: https://www.hxrmetal.com
- Address: Across from Sanjing Distillery on Road 4, Botou Economic Development Zone, Cangzhou City, Hebei Province
Copyright © 2026-2027 https://www.hxrmetal.com. All Rights Reserved. Hebei Haoxinran Machinery Manufacturing Co.,Ltd.