
- Site Navigation -
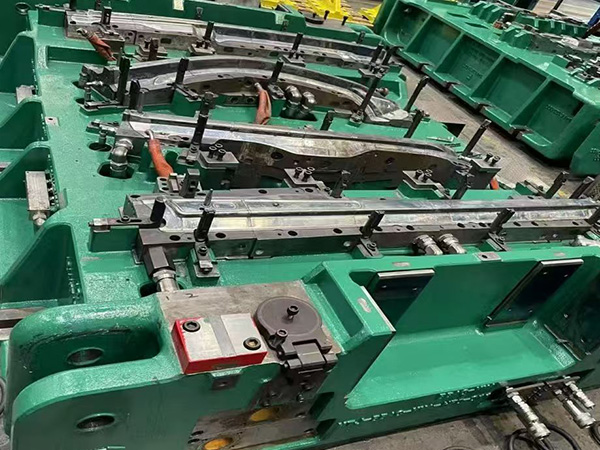
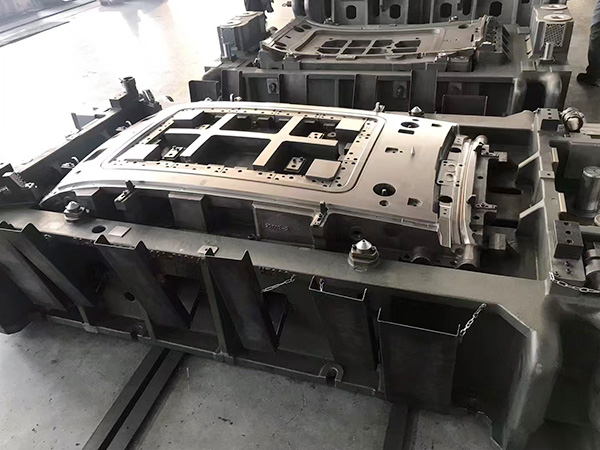
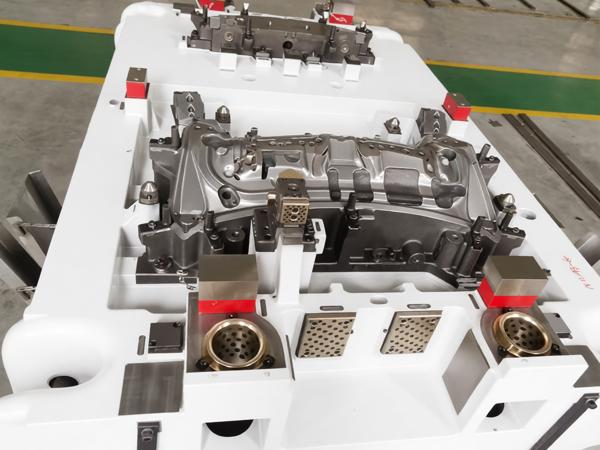
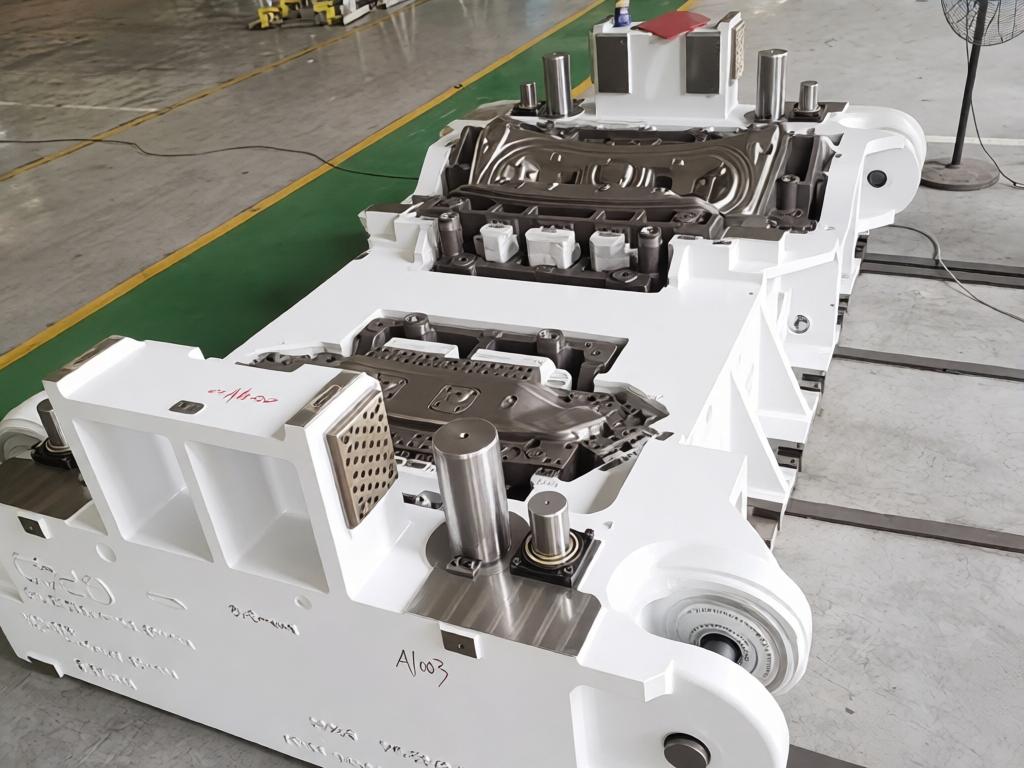
Wrinkling Defect Analysis and Control in Sheet Metal Stamping Dies
Date: 2026-09-21 10:58:55 Author: Haoxinran Views: 149 times
Wrinkling Defect Analysis and Control in Sheet Metal Stamping Dies
Wrinkling represents one of the most common and challenging defects in sheet metal stamping processes. Characterized by the formation of wavy folds in the material, wrinkling compromises part quality, dimensional accuracy, and tool integrity. This document provides comprehensive analysis of wrinkling mechanisms, prediction methods, and effective control strategies for stamping die design.
Wrinkling Mechanisms and Causes
1. Compressive Instability Theory
Wrinkling originates from compressive stress states that cause material buckling. When compressive stresses exceed critical thresholds, the thin sheet metal becomes unstable and forms wrinkles. The phenomenon is analogous to column buckling, where thin, flat surfaces fail under compression before reaching material yield strength.
2. Common Wrinkling Locations
Wrinkling typically occurs in specific areas of stamped components:
Flange areas: Wrinkles form in unsupported flange sections due to circumferential compression
Wall areas: Wrinkles develop in vertical walls during deep drawing operations
Blank holder regions: Wrinkling between binder surfaces when pressure is insufficient
Corner radii: Stress concentrations in tight radius areas promote wrinkling
3. Material and Process Factors
Multiple factors influence wrinkling tendency:
Material thickness (thinner sheets wrinkle more easily)
Material properties (yield strength, elastic modulus, strain hardening behavior)
Part geometry (draw depth, corner radii, surface area ratios)
Process parameters (blank holder force, draw bead geometry, lubrication conditions)
Wrinkling Prediction Methods
Analytical Prediction Models
Classical analytical models use buckling theory to predict critical wrinkling conditions. These models calculate critical compressive stress levels and compare them with actual process stresses to assess wrinkling risk.
Numerical Simulation
Finite element simulation provides detailed wrinkling prediction capabilities. Simulation can identify potential wrinkling areas, predict wrinkle severity, and evaluate the effectiveness of preventive measures before die construction.
Wrinkling Control Strategies
Blank Holder Force Optimization
Proper blank holder force application prevents wrinkling by maintaining sufficient compressive constraint on the material. Key optimization strategies include:
Applying sufficient but not excessive holding pressure
Using variable force profiles during the stamping cycle
Optimizing pressure distribution across the binder surface
Draw Bead Design
Draw beads control material flow and increase tension in critical areas. Strategic placement of draw beads prevents wrinkling by:
Increasing material tension in wrinkle-prone areas
Regulating material influx rates
Providing localized constraint against buckling
Process and Die Design Modifications
Additional wrinkling control measures include:
Increasing draw radii to reduce stress concentrations
Optimizing blank shape for better material distribution
Using intermediate forming operations for complex geometries
Implementing proper lubrication to control friction
Quality Control and Inspection
Wrinkling detection involves visual inspection, dimensional measurement, and surface quality assessment. Production monitoring tracks wrinkling frequency and severity to identify process drifts requiring adjustment.
Conclusion
Effective wrinkling prevention requires understanding of underlying material behavior, careful die design optimization, and precise process control. By applying the analysis and control strategies outlined in this document, stamping die designers can minimize wrinkling defects and improve overall production quality.
References
Sheet Metal Wrinkling Analysis - Material Science Research Publications
Deep Drawing Defect Prevention - Manufacturing Technology Standards
Finite Element Prediction of Wrinkling - Engineering Research Papers
Blank Holder Force Optimization - Process Control Guidelines
Contact Us
- Company Name: Hebei Haoxinran Machinery Manufacturing Co.,Ltd.
- Hotline: +86 18932785670
- Email: project@haoranmj.com
- Website: https://www.hxrmetal.com
- Address: Across from Sanjing Distillery on Road 4, Botou Economic Development Zone, Cangzhou City, Hebei Province
Copyright © 2026-2027 https://www.hxrmetal.com. All Rights Reserved. Hebei Haoxinran Machinery Manufacturing Co.,Ltd.